How to Choose the Best Thin Film Evaporator?
Choosing the best thin film evaporator requires more than comparing catalog capacities. The right unit must match your feed, target concentration, heat sensitivity, and production scale. A viscous polymer solution may need a different rotor design than a solvent-rich pharmaceutical stream. Small details matter.
Begin with the material itself. Record viscosity across operating temperatures, solids content, boiling range, fouling tendency, and residence-time limits. Ask suppliers for test data using a comparable feed, not only water or a simple solvent. A wiped-film or falling-film configuration can offer different heat-transfer behavior, cleaning demands, and product exposure. Review rotor speed, heating area, vacuum performance, seal design, and metallurgy together. Stainless steel may suit many processes, but corrosive compounds can require a more suitable alloy.
Practical experience also reveals weaknesses that brochures often hide. Inspect the discharge path, scraper condition, access doors, and condensate system. Calculate energy use at realistic loads. A unit that performs well at full capacity may struggle during frequent batch changes. That is easy to overlook. Confirm whether the manufacturer provides commissioning support, operator training, spare parts, and documented performance guarantees. Independent test results and references from similar facilities can strengthen your decision. Still, no selection method is perfect; feed behavior can change after installation. Plan a pilot trial, define measurable acceptance criteria, and leave room for adjustment. The best thin film evaporator is not simply the fastest machine. It is the one that delivers stable quality, manageable maintenance, and reliable results under your actual operating conditions.
Thin Film Evaporator Fundamentals and Operating Principles
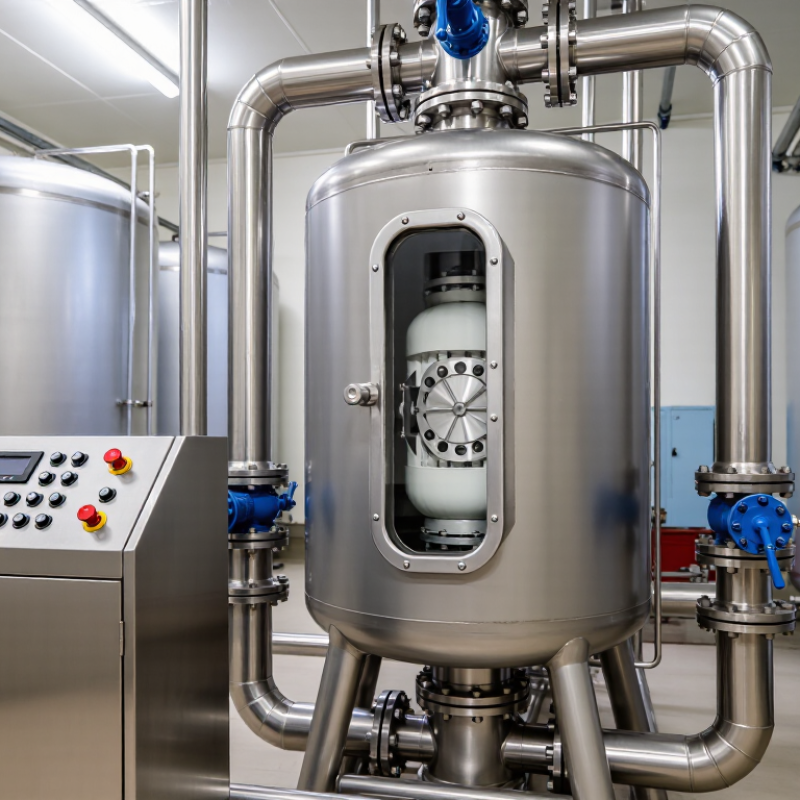
A thin film evaporator spreads liquid across a heated vertical wall. A rotating wiper creates a thin, turbulent film. Heat moves through the wall, while vacuum lowers the liquid’s boiling temperature. This reduces thermal stress on sensitive products. The U.S. Department of Energy’s Industrial Decarbonization Roadmap reports that process heating represents about 51% of energy use in U.S. manufacturing. Efficient film distribution therefore matters, not only for capacity, but also for energy control.
Selection should begin with feed behavior, not equipment size. Viscosity, solids content, foaming, fouling tendency, and heat sensitivity change the operating window. A short residence time can protect the product, yet excessive rotor speed may increase power demand and mechanical wear. The European Commission’s Best Available Techniques reference documents emphasize heat recovery, water reduction, and stable process control in evaporation-intensive industries. These principles are useful, but they do not replace pilot testing. A laboratory result may fail when feed composition shifts by only a few percent.
Tips: Confirm the required evaporation rate at the highest expected viscosity. Check vacuum performance under real vapor loads. Measure wall temperature, outlet solids, and residence time during trials. Select corrosion-resistant materials after reviewing chlorides, acids, and cleaning chemicals. Do not trust a perfect simulation. Real fouling is usually less polite. A practical choice balances heat-transfer area, rotor design, cleanability, maintenance access, and verified operating data.
How to Choose the Best Thin Film Evaporator?
Thin film evaporator selection depends strongly on operating pressure, thermal sensitivity, viscosity, and the required evaporation duty. The chart shows representative absolute pressure ranges for common evaporator configurations.
Lower pressure supports evaporation at reduced temperatures, which is important for heat-sensitive materials. Wiped-film systems are commonly selected for viscous or fouling feeds, while short-path systems are used when very low pressure and minimal thermal residence time are required. Actual operating conditions depend on feed properties, heat-transfer area, and process design.
Key Factors for Selecting a Thin Film Evaporator
Selecting a thin film evaporator starts with the feed, not the equipment brochure. Record viscosity, solids content, boiling range, and heat sensitivity at actual operating temperatures. A syrupy feed may need a larger wiping load than laboratory tests suggest. That detail matters. During practical trials, watch for wall build-up, unstable film flow, and product color changes. These observations often reveal more than a single throughput figure.
Residence time is a major selection factor for heat-sensitive materials. Choose a design that forms a uniform, thin film under controlled vacuum. Check evaporation rate, condenser duty, vacuum stability, and vapor carryover together. High vacuum can lower boiling temperature, but it will not correct poor distribution. Request test data using a comparable feed, including start-up, shutdown, and cleaning results. Independent testing or documented procedures can strengthen confidence. Scale-up is where assumptions fail.
Construction materials should match acidity, chlorides, solvents, and cleaning chemicals. Inspect rotor clearance, seal design, heating zones, access doors, and spare-part requirements. Operators also need clear controls for feed rate, jacket temperature, pressure, and rotor speed. Compare energy use per kilogram, not capacity alone. A compact unit may look efficient, yet frequent cleaning can erase that advantage. Review maintenance records from similar applications, then question results that seem unusually smooth. Reliable selection combines measured data, operator experience, and a pilot test that exposes real weaknesses.
Comparing Evaporator Designs, Materials, and Performance
Choosing the best thin film evaporator requires comparing design, material compatibility, and measured performance. In plant evaluations, I examine feed viscosity, heat sensitivity, solids content, and required evaporation rate. A wiped-film design suits viscous feeds and products that foul easily. Its rotating blades create a renewed surface and controlled residence time. A falling-film design can deliver higher throughput with lower mechanical complexity. However, it needs stable feed distribution and may struggle with highly viscous materials.
Material selection affects service life and product quality. Stainless steel is common, but the grade must match acidity, chlorides, temperature, and cleaning chemicals. Hastelloy-type alloys can improve corrosion resistance, though they increase capital cost. Surface finish also matters. Rough areas can trap residue. Seals and gaskets deserve equal attention; they often limit reliability before the heating surface does.
Small details matter.
Performance should be verified through heat-transfer coefficient, vacuum stability, energy use, residence time, and product recovery. Ask for test data under conditions close to your process. Laboratory results can look impressive. Full-scale behavior may differ. I have seen designs rated for high capacity lose efficiency when feed viscosity changed slightly. That is a useful warning, but not a universal rule. Maintenance access, spare-part availability, and cleaning time should enter the comparison. A slightly slower evaporator may prove more dependable when operators can inspect it quickly and adjust operating conditions safely.
Matching Evaporator Features to Process Requirements
How to Choose the Best Thin Film Evaporator?
Matching Evaporator Features to Process Requirements
Selecting a thin film evaporator starts with the feed, not the equipment brochure. Measure viscosity, solids content, thermal sensitivity, and expected throughput. A low-viscosity solvent mixture may need different rotor clearance than a thick polymer solution. Small details matter.
For heat-sensitive materials, choose a system with short residence time and accurate wall-temperature control. A wiped film design can spread the feed into a thin layer, improving heat transfer under vacuum. Confirm the required vacuum range with real process data. Pressure stability often affects product quality more than peak heating capacity.
Fouling risk also deserves close attention. Sticky feeds may require adjustable rotor speed, polished contact surfaces, and practical cleaning access. Check whether the heating zone, seals, and materials suit the chemicals used. Product recovery, vapor handling, and condenser capacity must match the evaporation load. Oversizing can increase cost and reduce control.
Pilot testing is valuable. Run representative feed material, not only a clean substitute. Record feed rate, wall temperature, pressure, rotor speed, and product color. I would not trust one successful trial. Feed composition can change during production. Recheck the design when solids, viscosity, or batch size changes. That reflection is easy to skip. It can prevent an expensive mismatch.
Installation, Operation, Maintenance, and Safety Considerations
Choosing the best thin film evaporator starts with the process, not the catalogue. Define feed viscosity, solids content, boiling temperature, residence time, and required throughput. A wiped-film design may suit heat-sensitive liquids, but only if the rotor, clearance, and heating surface match the feed. Small gaps matter.
The U.S. Department of Energy’s Industrial Decarbonization Roadmap reports that process heating uses about 51% of industrial energy. This makes heat-transfer efficiency a practical selection metric. Specify vacuum stability, condenser capacity, insulation quality, and controllable steam or thermal-fluid supply. IEA’s Energy Efficiency 2023 report places industry at roughly 37% of global final energy consumption, so inefficient evaporation quickly becomes expensive. During operation, operators should monitor pressure, wall temperature, motor load, feed rate, and vapor temperature. Trends reveal fouling earlier than a sudden product failure.
Installation needs level foundations, accessible seals, safe drainage, and correctly sized vacuum piping. Install relief protection and interlocks for loss of cooling, excessive pressure, and rotor overload. Keep hot surfaces guarded. Maintenance should include planned inspection of blades, bearings, seals, gaskets, thermocouples, and condenser tubes. Clean deposits before they harden; aggressive cleaning can damage surfaces and create leaks. The U.S. Chemical Safety Board repeatedly links inadequate management of change with serious process incidents, so altered feed properties deserve formal review. A perfect checklist does not replace judgment. In real plants, missed calibration is often more damaging than visible corrosion. Record every adjustment, even the minor ones.