Employment Application Apply
Global sourcing teams often choose a Sinle Layer Pcb when a product requires simple, reliable, and cost-conscious circuit design. This board uses one conductive copper layer, making production easier to understand and inspect. It suits LED controls, power modules, basic sensors, household devices, and educational electronics. Fewer layers can mean fewer alignment risks, shorter manufacturing cycles, and more predictable quotations.
The practical benefits become visible during supplier evaluation. Engineers can review trace widths, hole sizes, solder-mask quality, and material specifications with less complexity. Purchasing teams can compare factories using clear documents, approved samples, and inspection records. A capable supplier should provide material certificates, production tolerances, electrical testing details, and evidence of compliance with destination-market requirements. These details matter when boards cross borders and enter regulated supply chains.
But simple does not mean automatically better. That assumption can be wrong. A single-layer layout may require longer traces, wire links, or extra components. Those changes can increase assembly time and reduce product compactness. Based on sourcing experience, the right decision depends on circuit density, operating environment, order volume, and expected service life. Teams should test prototypes before committing to large production. They should also confirm packaging protection, moisture control, labeling, and change-management procedures. A low initial price is attractive, but stable quality and documented communication usually protect the total cost. The board looks simple. The sourcing decision is not.
Why Choose Single Layer PCB for Global Sourcing?
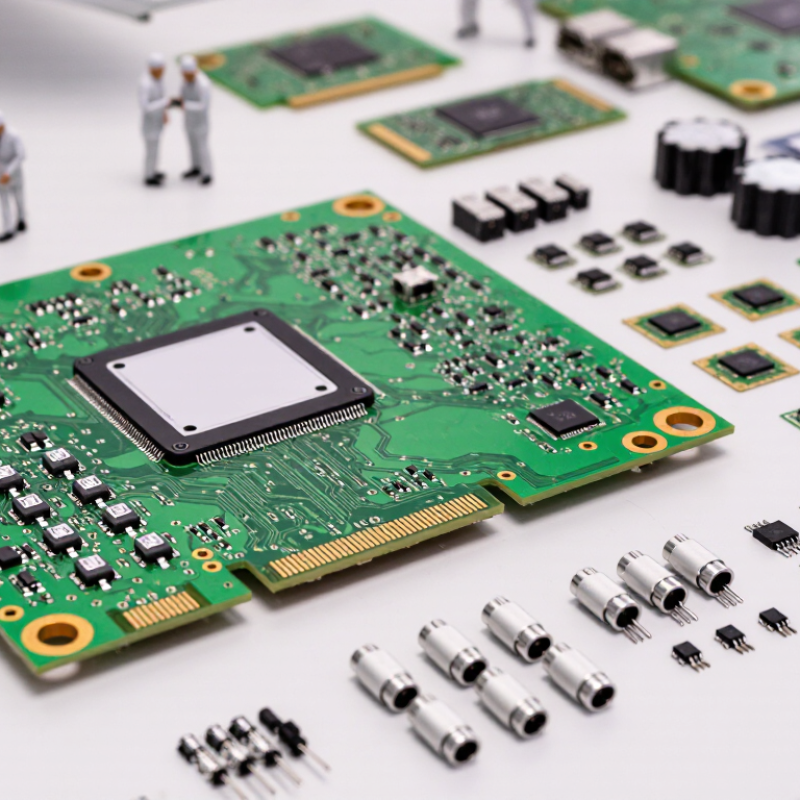
A single-layer PCB uses one conductive copper layer bonded to an insulating substrate. The copper surface carries current between components, pads, and connection points. A protective solder mask covers unused copper and helps prevent accidental shorts. Printed markings identify component positions during assembly and inspection.
Its operating principle is straightforward. Current enters through a connector or terminal, follows etched copper traces, and reaches each component. Resistors, capacitors, and diodes then perform their assigned electrical functions. Through-holes allow components to pass through the board and connect with the copper layer. The structure is easy to inspect. It is also easier to repair when a trace fails.
That simplicity supports global sourcing. Suppliers can produce these boards with fewer fabrication steps, shorter inspection routines, and clearer quality records. In practical procurement work, buyers should verify copper thickness, substrate grade, hole accuracy, solderability, and electrical continuity. A low price alone proves little. Poor trace spacing can create faults, especially near power paths. Single-layer designs also need more physical space than multilayer boards. That limitation is easy to underestimate. For compact or high-density equipment, this structure may not be the best choice. Even so, for control panels, basic sensors, lighting circuits, and simple power devices, its visible layout makes production checks more reliable across different manufacturing locations.
Single-layer PCBs use one conductive copper layer on a nonconductive substrate. Their simple structure supports straightforward routing, easier inspection, and efficient sourcing for low-density electronic circuits.
Operating principle: Components are mounted on the board, while copper traces on the single conductive layer connect pads and complete electrical circuits. Compared with multilayer designs, the reduced layer count can simplify fabrication, visual inspection, documentation, and supplier qualification.
For global sourcing, single-layer PCBs offer a clear cost and production advantage. Their structure uses one conductive copper layer, reducing drilling, lamination, and inspection steps. This simpler process can shorten supplier qualification. It also makes quotations easier to compare across regions. IPC’s 2023 World PCB Production Report valued global PCB output at approximately 89.7 billion dollars in 2022. In such a large market, small process savings can influence total landed cost.
Single-layer boards suit lighting controls, basic power circuits, sensors, and household interfaces. Their open layout supports faster visual inspection and simpler repair work. A procurement team can often approve samples with fewer technical questions. That matters when engineers, factories, and buyers work across different time zones. IPC’s 2024 PCB Technology Roadmap emphasizes manufacturability, material availability, and supply-chain resilience as continuing industry priorities. Single-layer designs support those priorities with widely available materials and familiar equipment.
The trade-off is real. Routing space becomes limited, and complex circuits may need another board structure. Do not force simplicity. In sourcing reviews, I would check current, heat, hole size, and insulation distances before choosing a supplier. A low unit price can hide higher assembly or testing costs. That assumption deserves scrutiny. Designers should also confirm regional material standards and packaging conditions, especially after long ocean transit. A practical drawing, stable specifications, and measurable acceptance criteria usually matter more than a promising quotation.
Single-layer PCBs remain practical for many cost-sensitive electronic products. Their simple structure supports easier sourcing, clearer specifications, and faster production communication. Material selection still requires care. FR-4 is common because it offers stable insulation and moderate heat resistance. For less demanding products, lower-cost substrates may be suitable. However, they can show greater warping or weaker dimensional stability. Copper weight also affects current capacity and heat performance. I have seen small traces overheat when designers focused only on board price.
Manufacturing is simpler, but not careless. Fewer conductive layers reduce alignment risks and shorten inspection routes. Reliable suppliers should control drilling, etching, solder-mask coverage, and board flatness. Ask for process capability data, not vague quality promises. A complete drawing should specify dimensions, tolerances, hole sizes, copper thickness, and surface finish. During sampling, inspect actual panels rather than trusting photographs. Panel utilization can also affect the final cost.
Quality depends on measurable acceptance criteria. Check board dimensions, hole accuracy, copper thickness, insulation resistance, and surface appearance. Keep approved samples and inspection records for repeat orders. Packaging deserves attention too. Moisture barriers and corner protection can prevent damage during long-distance transport. I would not assume a visually clean board is electrically reliable. Some defects appear only after assembly or thermal cycling. Rechecking those conditions may feel excessive, but it can expose weak material choices before production expands.
Why Choose Single Layer PCB for Global Sourcing?
Cost, Supply Chain, and Production Efficiency Factors
Single-layer PCBs often reduce global sourcing costs through simpler fabrication. They require fewer lamination steps, fewer drilled connections, and shorter inspection cycles. That simplicity can lower tooling costs and shorten quotation time. IPC industry data consistently shows that material and labor pressures strongly influence PCB pricing. A simpler structure gives purchasing teams more room to negotiate.
Supply chain reliability also matters. UNCTAD reports that more than 80% of global merchandise trade by volume moves by sea. Fewer process stages can reduce production delays before shipping begins. Standardized board dimensions, common copper weights, and widely available substrates support multi-region sourcing. This helps when one supplier faces capacity problems. It is not risk-free.
Production efficiency becomes visible on the factory floor. Operators can inspect one conductive layer more quickly than a complex multilayer design. Automated optical inspection also faces fewer routing relationships. The IPC Global Sentiment of the Electronics Industry reports continued concern about component availability, labor, and manufacturing costs. Single-layer designs cannot solve every constraint, but they can remove unnecessary process complexity.
The trade-off deserves attention. A single-layer board needs more physical space for routing. It may also require wire links or a larger enclosure. Engineers sometimes choose it too early. That mistake can increase assembly costs later. A practical sourcing review should compare total delivered cost, not only the quoted board price. Sample testing, regional lead-time checks, and yield data make that comparison more reliable.
| Evaluation Dimension | Single-Layer PCB | Two-Layer PCB | Four-Layer PCB | Global Sourcing Implication |
|---|---|---|---|---|
| Typical Construction | One copper layer on one side of the insulating substrate; components are generally mounted on the copper side. | Two copper layers separated by an insulating core, with plated through-holes connecting the layers. | Four copper layers separated by dielectric material and bonded in a multilayer stack-up. | Lower construction complexity generally means easier supplier qualification and simpler incoming inspection. |
| Relative Bare-Board Cost | Lowest baseline cost; commonly used as the cost index of 1.00. | Typically about 1.3–2.0 times the cost of a comparable single-layer board. | Typically about 2.0–4.0 times the cost of a comparable single-layer board. | Single-layer designs are most attractive when routing and electrical requirements do not require additional copper layers. |
| Material Consumption | Uses one copper foil layer and a relatively simple laminate structure. | Uses two copper foil layers, additional dielectric material, and plated interconnections. | Uses multiple copper foils, dielectric layers, bonding materials, and a controlled multilayer stack-up. | Lower material usage can reduce exposure to copper, laminate, and chemical-processing price fluctuations. |
| Manufacturing Process Steps | Fewer imaging, plating, lamination, drilling, and registration steps. | Requires additional alignment, drilling, plating, and registration controls. | Requires lamination, multilayer registration, sequential processing, and tighter process control. | Fewer process steps can reduce manufacturing risk and make production easier to transfer between qualified suppliers. |
| Common Production Lead-Time Range | Approximately 3–7 working days for standard prototypes or repeat production, excluding shipping. | Approximately 5–10 working days for standard prototypes or repeat production, excluding shipping. | Approximately 7–15 working days for standard prototypes or repeat production, excluding shipping. | Shorter fabrication cycles can support faster replenishment and reduce the need for high finished-goods inventory. |
| Design and Routing Capability | Best for simple circuits with low routing density and limited interconnection requirements. | Supports routing on both sides and is suitable for moderately complex control and interface circuits. | Supports higher routing density, ground or power planes, controlled impedance, and more complex signal distribution. | Single-layer boards are cost-effective only when the circuit can meet electrical and layout requirements without extra layers. |
| Component Density | Low to moderate; limited by one-sided routing and available board area. | Moderate to high; components and traces can use both sides of the board. | High; internal planes and multiple routing layers improve space utilization. | For compact products, a higher layer count may reduce enclosure size enough to offset the higher board price. |
| Quality-Control Complexity | Lower inspection complexity, with fewer layer-registration and interconnection variables. | Moderate; requires control of plated holes, layer alignment, and solderability on both sides. | Higher; requires tighter control of lamination, internal connections, registration, and potential delamination risks. | Simpler inspection can reduce supplier-audit effort and improve consistency across multiple production locations. |
| Yield and Rework Exposure | Generally lower process-related defect exposure because the construction is simpler. | Moderate process exposure, especially around plated through-holes and layer registration. | Higher process exposure because defects may occur inside the board and be difficult to rework. | For high-volume, price-sensitive products, a simple board can lower scrap and rework costs when performance requirements permit. |
| Supplier Availability | Broadly available from standard PCB fabricators in major manufacturing regions. | Broadly available, although capability requirements vary by material, finish, and design rules. | Widely available but more dependent on advanced equipment, engineering controls, and qualified process capability. | A larger qualified supplier pool can improve quotation coverage, negotiation leverage, and continuity planning. |
| Shipping and Inventory Effect | Lower unit value and shorter production time can reduce safety-stock requirements for stable demand. | Moderate unit value and production time; inventory planning depends on demand variability and order quantities. | Higher unit value and longer fabrication time may justify larger safety stocks for critical products. | Single-layer boards can support leaner inventory strategies when demand is predictable and the design is mature. |
| Best-Fit Applications | LED products, basic power supplies, relays, sensors, simple controllers, and low-density consumer or industrial devices. | Control panels, communication interfaces, moderate-density embedded systems, and general-purpose electronics. | Processors, high-density digital systems, RF designs, complex industrial controls, and products requiring power or ground planes. | Select the lowest layer count that satisfies routing, thermal, mechanical, reliability, and regulatory requirements. |
Single-layer PCBs suit circuits with modest routing needs and stable electrical behavior. Common applications include LED lighting, relay controls, battery chargers, alarm panels, and basic sensor modules. They also work well in educational kits and low-frequency analog devices. A visible copper side makes inspection easier. Through-hole components can be repaired with basic tools.
Selection should begin with circuit density, not price alone. Check whether every trace fits on one copper layer without unsafe crossings. Measure expected current, operating voltage, and heat near power components. For example, a 2 mm power trace may be insufficient for a high-current load. Copper thickness, board size, hole diameter, and material grade also affect reliability. In humid environments, surface protection and suitable solder mask deserve attention. A single layer is not automatically better.
Global sourcing requires clear fabrication documents. Specify tolerances, drill data, surface finish, testing method, and packaging conditions. Ask for sample inspection before approving volume production. Examine edge quality, solderability, and trace width under magnification. Production reviews often reveal small problems, such as silkscreen marks covering a reference point. That detail can slow assembly. Cost comparisons should include tooling, freight, inspection, and possible rework. Sometimes a two-layer design becomes more practical after routing is reviewed honestly. Even then, the single-layer option remains valuable when simplicity, repair access, and controlled production are the real priorities.